
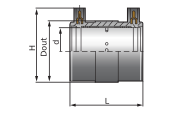
Electrofusion socket straight, PertFlextra
Component Number:
1018
Applicable Systems:
The FlexPipe
Description
Electrofusion sockets with built-in electric heating elements for joining PE-RT service pipes by electrofusion welding.
Each item is packed in a plastic bag. The plastic bag is packed in a cardboard boxes.
To be stored dry and protected from direct sunlight.
The body of each electrofusion socket is marked with:
- Nominal diameter
- PE-RT II
- Production date
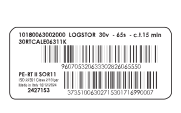
From the label on each electrofusion socket the following information appear:
- A bar code to be scanned by a standard welding unit
- Manufacturer’s product No./fitting code
- ISO 22391
- Class 2/10 bar
- Welding voltage (V)
- Welding time (seconds)
- Cooling time (seconds or minutes)
- Production traceability code
Application
Used to connect PE-RT service pipes.
Maximum design pressure according to EN17878-2: 10 bar.
Standard welding machines for electrofusion sockets are used to install electrofusion sockets.
LOGSTOR recommends that the fitter who installs electrofusion sockets have completed relevant courses and is certified according to national standards for plastic welding, as it can be essential for the quality and service time of the system. Certificates include i.a. the following:
- Theoretical knowledge about plastic welding techniques and materials
- Practical skills as regards different welding methods
- Safety precautions and quality control
- Plastic welding certificates must be renewed periodically, and may require that the welder demonstrates updated knowledge and skills
LOGSTOR can hold a 1-day course about installation of an electrofusion socket on PE-RT. The course does not give a certificate according to national requirements to plastic weldings as mentioned above, but will cover the following
- Removal of insulation from PertFlextra
- Removal of protection layer and diffusion barrier
- LOGSTOR electrofusion socket programme incl. description of its materials
- Tools for welding electrofusion sockets
- Preparations for welding
- Welding electrofusion sockets
- Documentation